

Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat
Engineered for robust mechanical handling, micro-particle isolation, and fluid recovery across drilling and specialized chemical synthesis.
The fundamental science of solid-liquid phase separation, hydrodynamic shearing, and continuous slurry classification has long anchored heavy energy drilling. Today, the core mechanical principles powering modern solids control systems for oil drilling are catalyzing major technological breakthroughs in precision chemical manufacturing, particularly in the synthesis and purification processes vital for optical films and precision electronic coatings. As optical display panels, semiconductor packaging, and microelectronic devices demand defect-free surfaces down to single-digit nanometer tolerances, the upstream purification of raw resins, polymer slurries, and carrier fluids relies on mechanical separation concepts pioneered in industrial drilling fluid engineering.
In conventional oilfield operations, drilling mud serves as the hydraulic lifeline—circulating cuttings, stabilizing subterranean pressure, cooling drill bits, and maintaining chemical balance. A robust solids control system systematically removes drilled solids through staged mechanical processes involving shale shakers, degassers, desanders, desilters, and high-speed decanting centrifuges. Similarly, precision electronic coating formulations—such as anti-reflective films, polarizing layers, multilayer ceramic capacitors (MLCC), and photoresist precursors—require rigorous de-agglomeration, particle size classification, and continuous suspension homogenization to eliminate abrasive contaminants and micro-bubbles that cause optical distortion or electrical breakdown.
Iterative screening cascades from coarse mechanical separation to high-G centrifugal decantation, isolating critical particle fractions while preserving valuable liquid phases.
Dynamic mechanical agitation and non-destructive pumping stabilize non-Newtonian slurries, preventing premature sedimentation and shear-induced polymer degradation.
Zero-discharge engineering principles minimize chemical waste, reclaim expensive solvents, and protect delicate cleanroom and industrial environments.
The commercial landscape for precision coatings has expanded exponentially with the rapid rise of flexible OLED displays, autonomous vehicle optical sensors, fifth-generation (5G) dielectric substrates, and lithium battery separator films. In these advanced manufacturing ecosystems, coating slurries consist of functional nano-scale ceramics, organic dyes, transparent conductive oxides (TCO), and polymer binders dispersed within specialized organic solvents. Contaminants such as oversize agglomerates, metal wear particles, and insoluble gels can ruin an entire production batch, resulting in pinhole defects, optical haze, or localized dielectric failure.
Adapting high-capacity, heavy-duty solids control technologies provides a scalable solution for high-throughput slurry preparation. For instance, high-shear mud mixing systems and heavy-duty mud agitators offer the precise fluid dynamics necessary to dissolve difficult polymers and wet out ultrafine pigments evenly. Hydrocyclone desanders and desilters, long utilized to remove 15-to-75 micron abrasives from drilling mud, provide high-volume pre-filtration for bulk chemical feedstocks, significantly extending the operational lifespan of downstream sub-micron membrane filters.
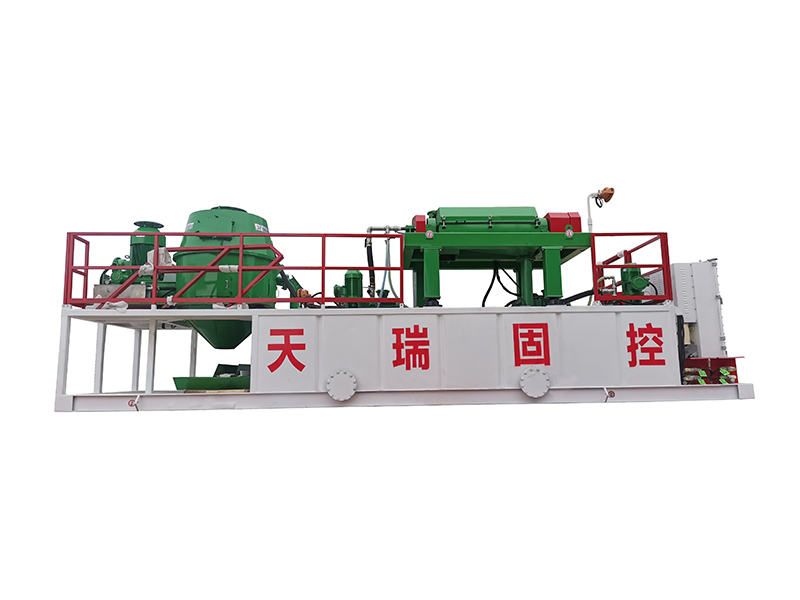
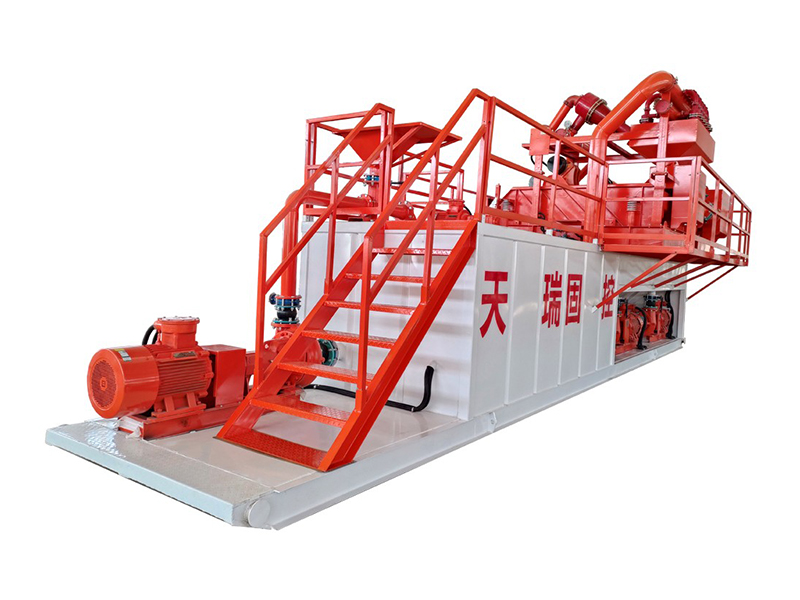
A comprehensive solids control system functions as a tightly integrated closed loop. When adapted for advanced material processing and petrochemical feed purification for optical substrates, each piece of equipment serves a specialized classification and processing function:
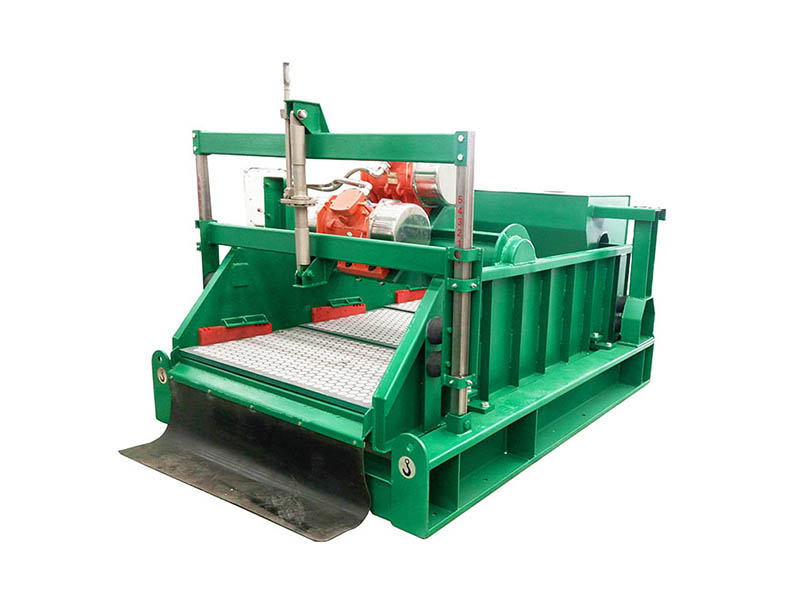
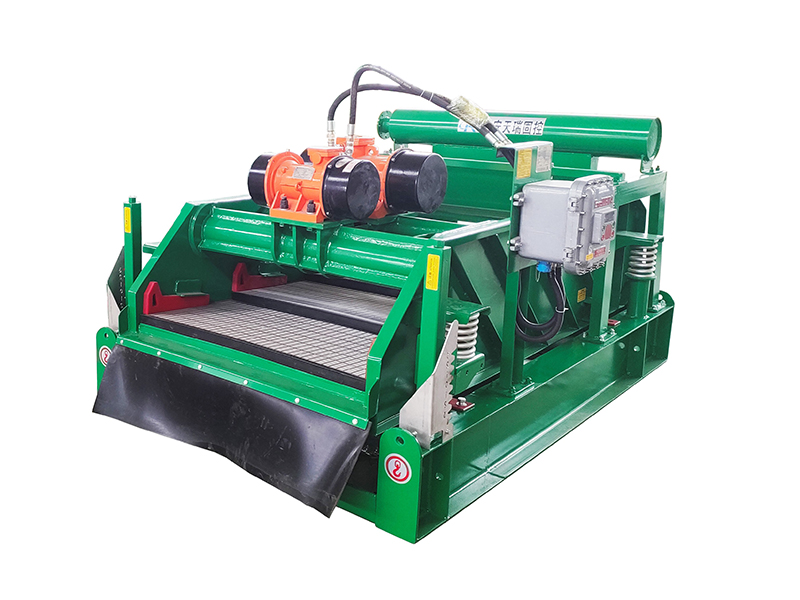
In oilfield operations, linear and balanced elliptical motion shale shakers utilize high gravitational accelerations (up to 7.5G - 8.2G) to shear non-Newtonian drilling fluids through high-tension wire mesh screens, discarding bulk solids while retaining drilling mud. In chemical slurry refinement, advanced vibration mechanics enable high-viscosity coating resins to flow through ultra-fine mesh without blinding or cake compaction, efficiently separating raw particulate matter and unreacted granulates.
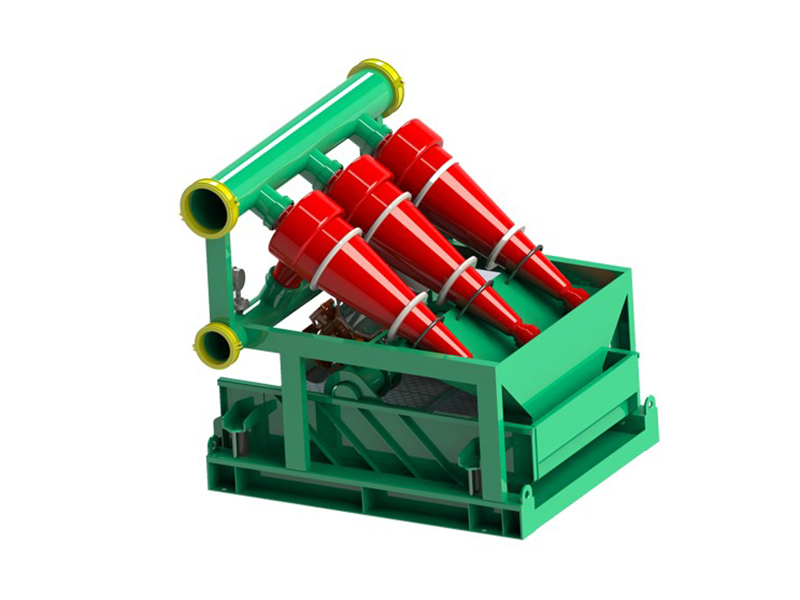
Hydrocyclones leverage centrifugal acceleration generated by pressurized involute fluid feeds. Desanders isolate solids between 45 and 74 microns, while desilters classify particulates down to 15 microns. In the production of raw optical film polymers and industrial solvent recycling, hydrocyclone separation eliminates coarse abrasive sand and pipeline scales, ensuring fluid clarity prior to fine milling.
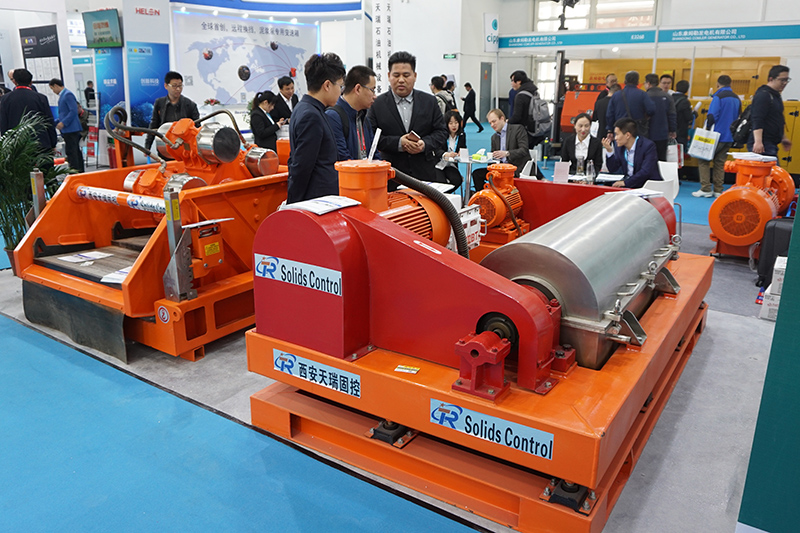
Operating at rotational speeds exceeding 3,000 RPM and generating centrifugal forces above 2,500G, decanter centrifuges achieve continuous separation of colloidal suspensions and fine solids down to 2 to 5 microns. In electronic coating waste management and solvent reclamation, decanters separate pigment slurries and binder residues, enabling closed-loop solvent recycling and drastically reducing hazardous waste disposal.
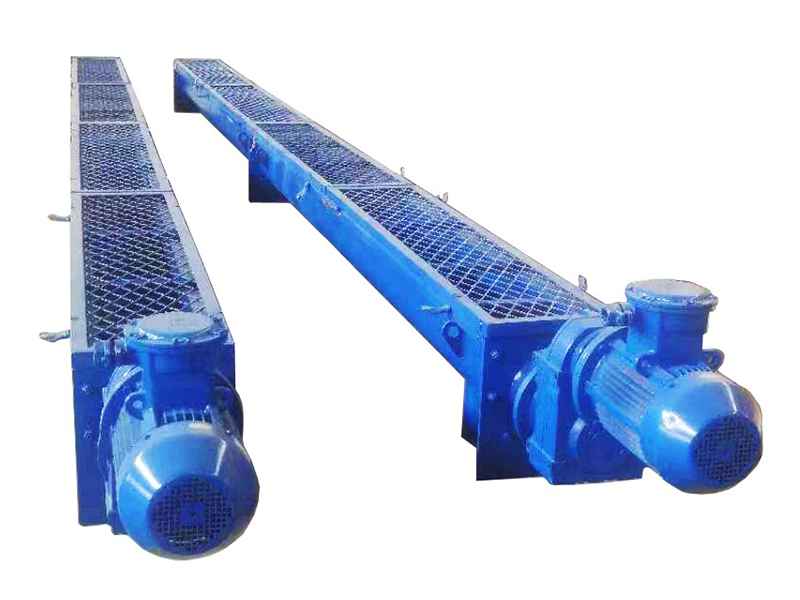
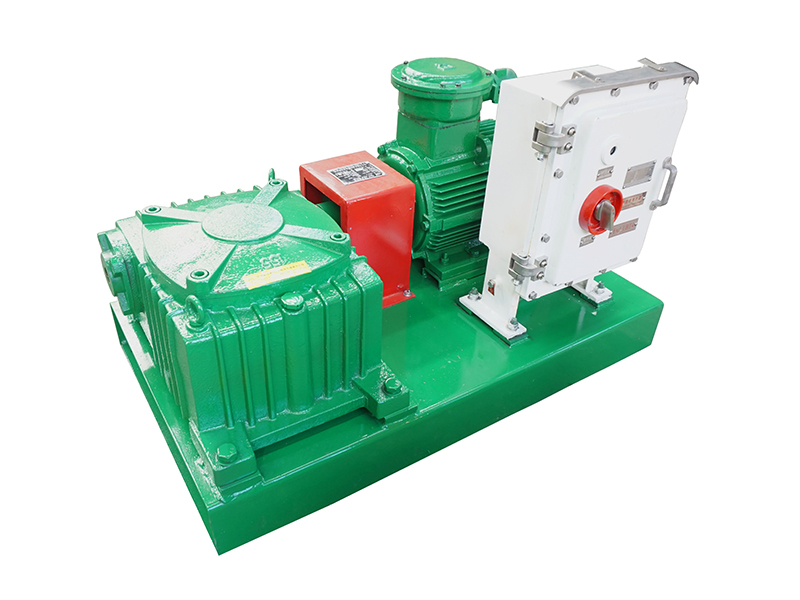
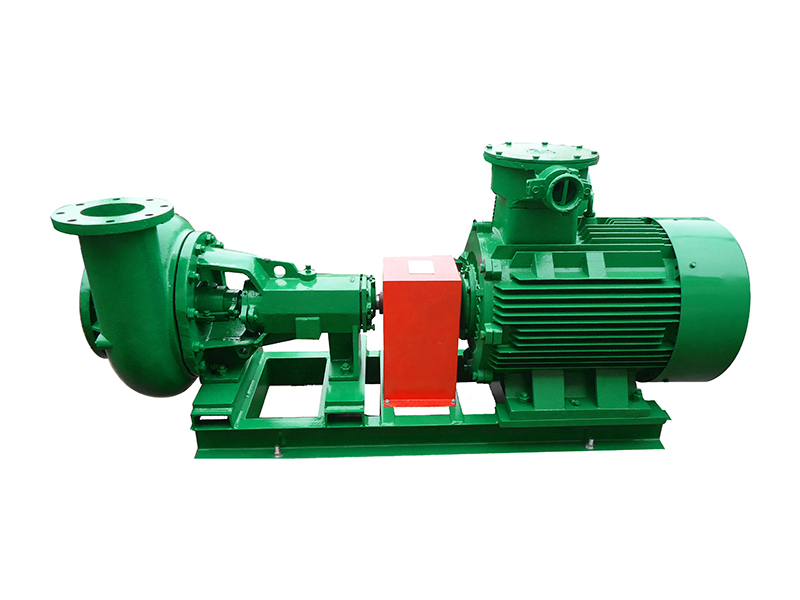
Uniform dispersion is paramount in preventing phase stratification. Industrial mud agitators equipped with turbine impellers create axial and radial fluid currents within storage tanks. When paired with screw conveyors and progressive cavity pumps that deliver low-shear fluid transfer, delicate emulsions and optical slurries are transported without droplet fragmentation or bubble entrainment.
The future of solids control systems across drilling, optical film substrate refining, and precision coating lines is being reshaped by three transformative macro trends:
Intelligent Digital Sensing & AI Automation: Modern solids control units are increasingly equipped with integrated IoT vibration sensors, inline acoustic viscosity meters, and automated choke valves. Machine learning algorithms analyze real-time density and particulate distribution, dynamically adjusting shaker deck angles, screen basket frequencies, and centrifuge differential speeds to optimize separation cut-points without human intervention.
Green Chemistry and Sustainable Solvent Recovery: Both oilfield operators and electronic chemical manufacturers face stringent environmental regulations governing VOC emissions and hazardous waste streams. Next-generation oil-based mud recycling systems and closed-circuit vapor recovery units eliminate fugitive emissions while achieving solvent recovery rates exceeding 95%, reinforcing corporate environmental, social, and governance (ESG) commitments.
Ultra-Pure Material Demands in Semiconductor & Display Sectors: As semiconductor nodes shrink below 3nm and optical films integrate multi-functional anti-glare, anti-smudge, and refractive properties in sub-micron thickness layers, the tolerance for slurry impurities approaches zero. Upstream industrial filtration systems capable of high-throughput primary purification ensure that downstream chemical synthesis operates under pristine conditions.
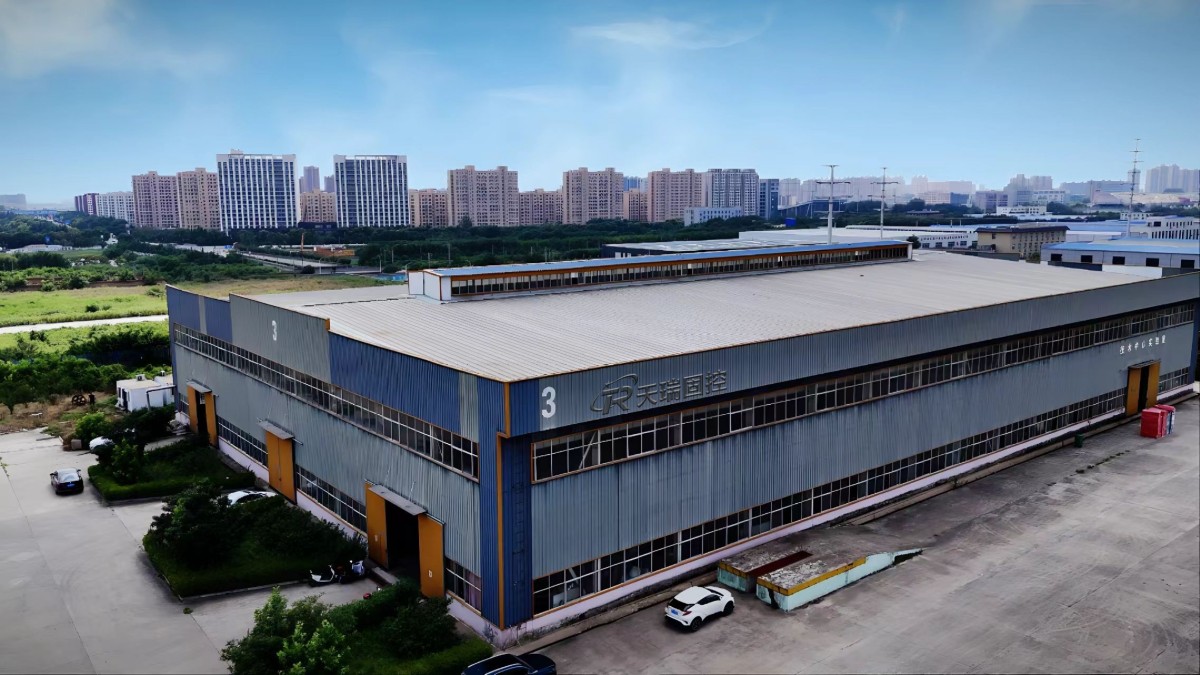
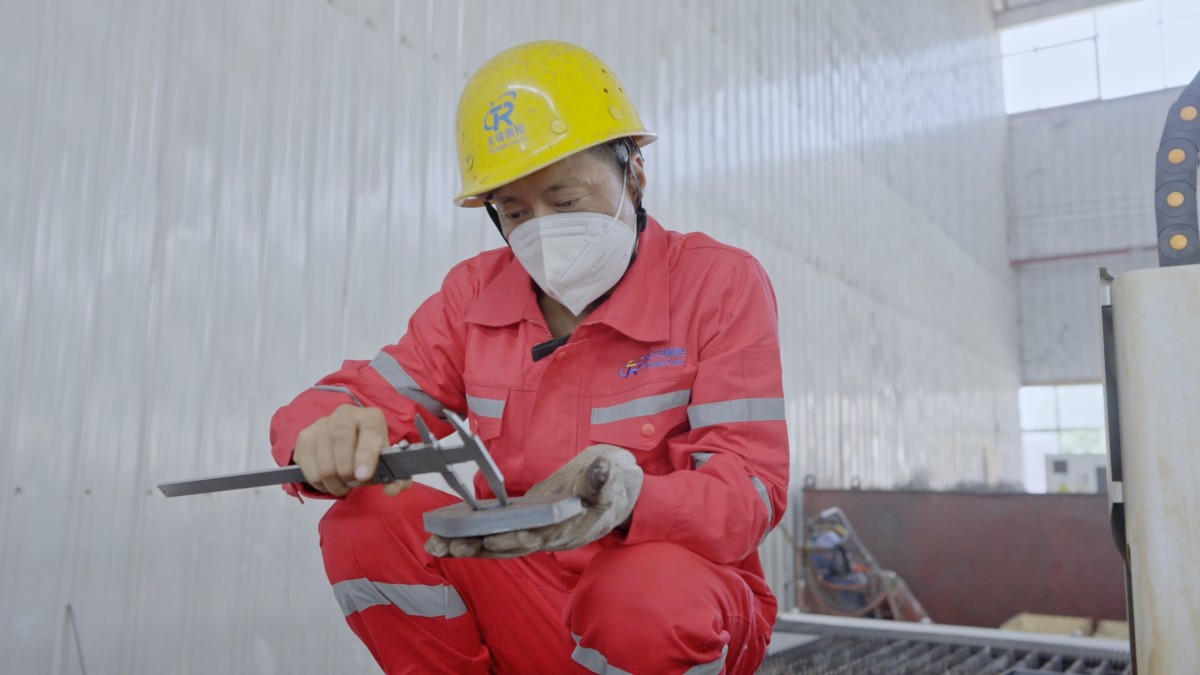
Established in 2010, TR Solids Control is a professional manufacturer specializing in drilling fluid solids control equipment and integrated solutions. We are dedicated to the design, manufacture, sales and services of solids control systems, following strict quality standards and providing reliable products, professional support and fast response for global customers.
During the past years, together with our experienced engineering team and strong supply chain partners, we have supported drilling contractors, oilfield service companies and industry partners across Middle East, Africa, Russia, South America, Southeast Asia and other regions, delivering efficient solids control solutions for various drilling operations.
From complex oil and gas drilling sites to heavy trenchless civil engineering and precision industrial fluid treatment, our equipment is built to operate under demanding environmental conditions worldwide.
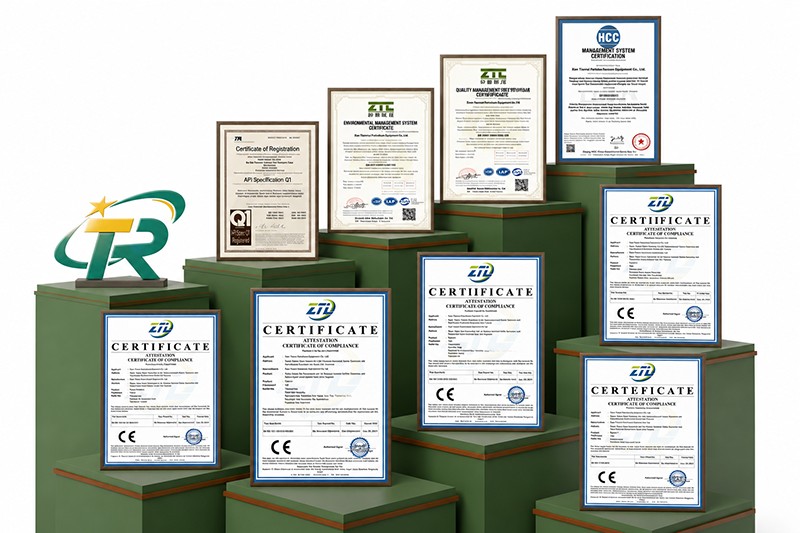
State-of-the-art facilities, certified quality management systems, and a consistent international footprint.
Full-spectrum equipment line designed for high performance, continuous fluid recovery, and rigorous solids management.