

Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat
Engineered to satisfy North American strict environmental zero-discharge mandates and heavy-duty drilling cycles with high efficiency, robust wear resistance, and modular skid configurations.
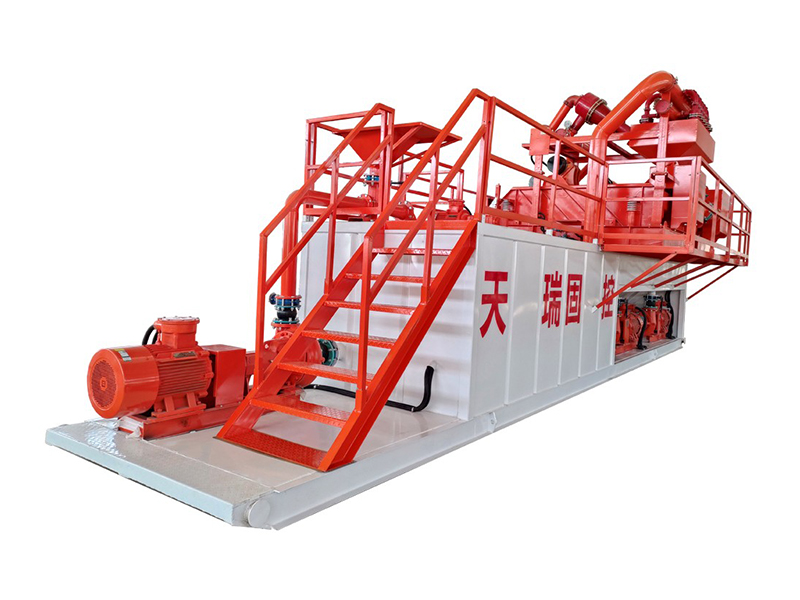
Compact closed-loop desanding and desilting mud recycling station engineered for US horizontal directional drilling, river crossings, and civil infrastructure projects.
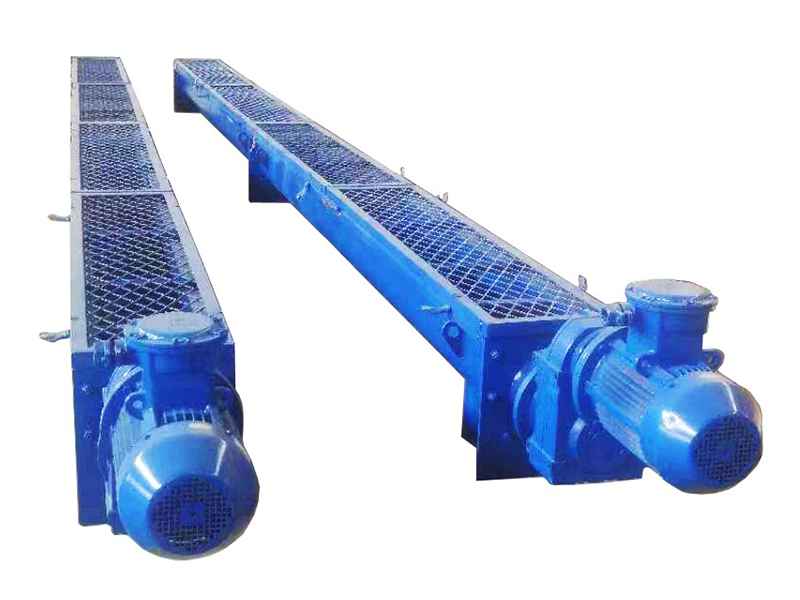
Heavy-duty auger conveyor with explosion-proof electric drive, optimized for non-stop mud cake and shale shaker discharge conveyance on US land rigs.
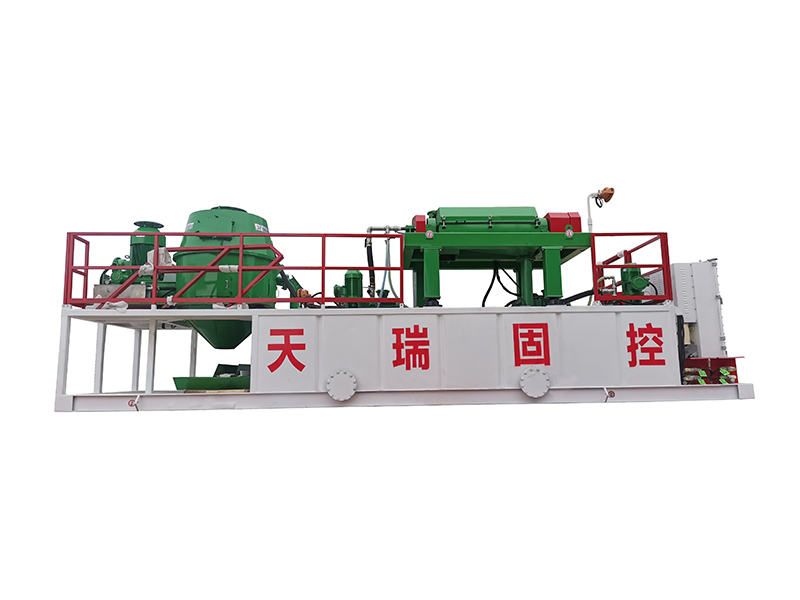
Advanced vertical cuttings dryer and centrifuge combination recovering up to 95% base oil to meet stringent US EPA and Texas RRC waste compliance standards.
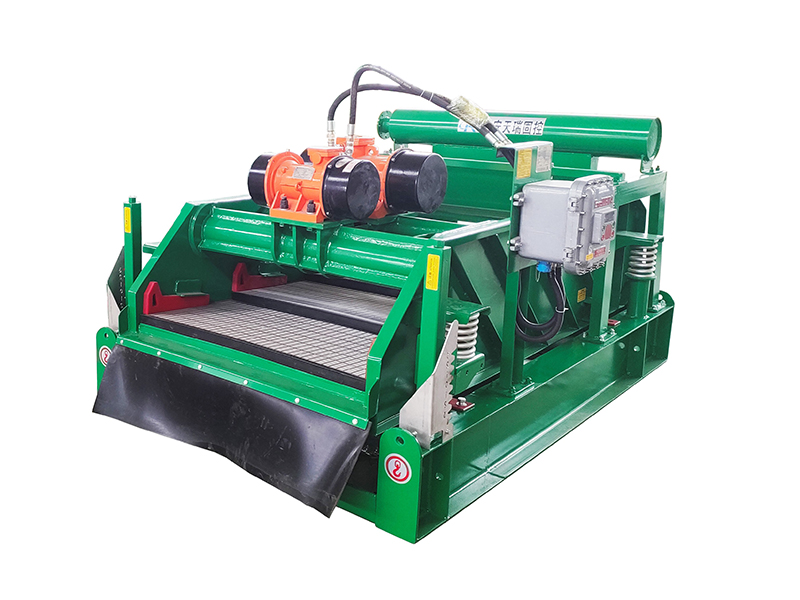
Multi-deck primary solids separation unit with adjustable vibration intensity up to 7.5G, designed to process high-viscosity drilling fluids in unconventional shale wells.
The United States oil and gas industry remains the global benchmark for technical innovation, operational velocity, and rigorous environmental stewardship. Across unconventional tight oil and shale gas plays—most notably the Permian Basin (Midland and Delaware Basins), Eagle Ford, Bakken Formation, Haynesville, and the Marcellus/Utica shales—drilling operators utilize ultra-long lateral horizontal wells that exceed 10,000 to 15,000 feet. These extended-reach drilling (ERD) programs generate massive volumes of abrasive fine solids and require uninterrupted mud circulation systems capable of maintaining precise rheological properties under severe dynamic loads.
In this intensive operational setting, an oilfield solids control system is no longer a standard mechanical accessory; it is the vital operational core of the drilling rig. The presence of low gravity solids (LGS) not only increases mud weight unnecessarily but also causes excessive drill bit wear, pipe sticking incidents, formation damage, and exponential spikes in chemical additive costs. US drilling contractors and mud engineering firms demand rugged, API-compliant, and high-efficiency solids control solutions that deliver ultra-clean mud recycling while minimizing total drilling waste volumes.
With tightening environmental surveillance by the US Environmental Protection Agency (EPA) and state commissions such as the Texas Railroad Commission (RRC) and New Mexico OCD, operators must eliminate open reserve pits. Closed-loop mud systems and drilling waste recovery units reduce liquid discharge and prepare clean cuttings for beneficial reuse or thermal desorption.
In lateral shale intervals, oil-based mud (OBM) and synthetic-based mud (SBM) provide superior lubricity and borehole stability. Because base oils represent significant operational capital, recovering synthetic fluids through high-G decanter centrifuges and vertical cuttings dryers yields direct payback for US operators.
Modern US drilling contractors prioritize automated mud properties monitoring, predictive motor diagnostics, and variable-frequency drive (VFD) controls. Our systems integrate smart sensors that interface directly with rig centralized PLC scada platforms.
Our integrated mud circulation and solids control packages utilize systematically balanced multi-stage hydro-mechanical equipment to progressively isolate and remove drilled solids down to 2 microns.
Equipped with linear and balanced elliptical motion trajectories, our shale shakers handle flow rates over 500 GPM per unit, capturing coarse drill cuttings down to 74 microns (API 200 mesh) without premature screen blinding or fluid loss over the header box.
Removes entrained formation gases (methane, H2S, CO2) rapidly to restore drilling mud specific gravity, stabilize feed pump suction pressure, and eliminate dangerous well control kick risks on live oilfield assets.
Utilizing wear-resistant pure polyurethane hydrocyclone cones (10" & 12" desanders for 45-74 micron cut points; 4" desilters for 15-44 micron separation), equipped with bottom underflow drying shakers for dry cake discharge.
Operating at G-forces exceeding 3000G with variable drum and screw differential speeds to strip colloidal clays (2-7 microns) and execute selective barite recovery, preserving valuable weighting materials while clarifying active mud.
Heavy-duty mud agitators and venturi mixing hoppers provide non-stop fluid agitation in active mud tanks, preventing weighting agent settling, mud dead-zones, and uneven polymer hydration across cold weather conditions.
Automated chemical dosing units combined with high-volume decanters flocculate ultra-fine particulates, generating crystal-clear reusable process water and dry stackable solids for rapid site remediation.
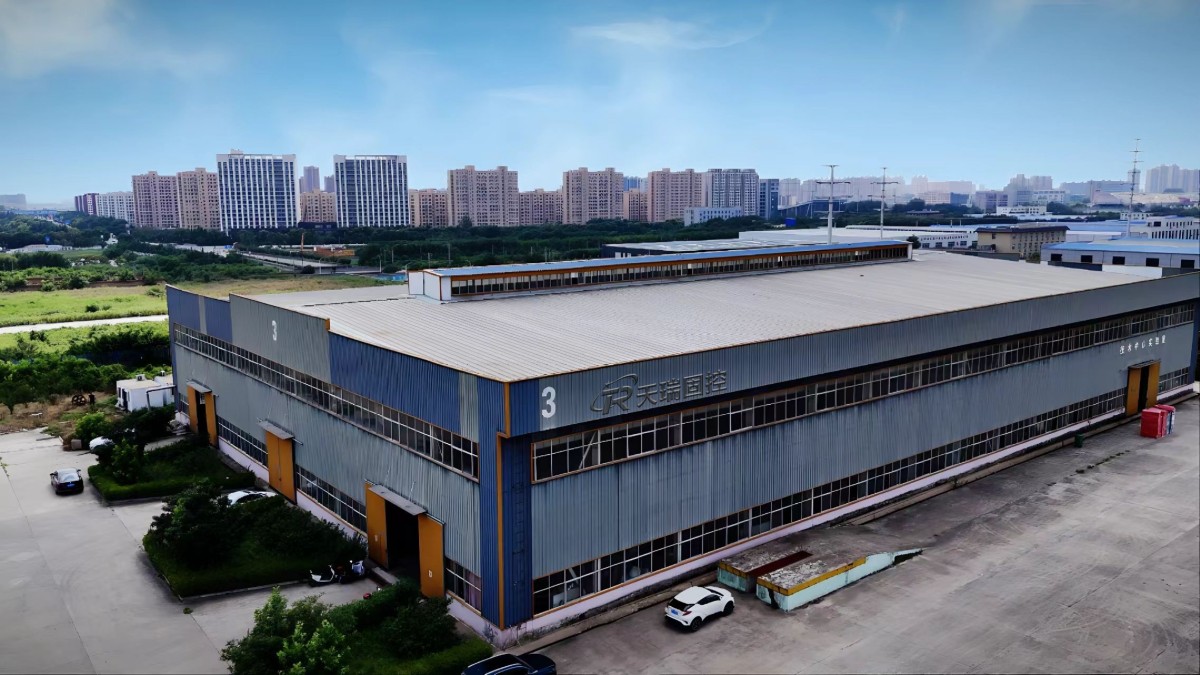
Established in 2010, TR Solids Control is a professional manufacturer specializing in drilling fluid solids control equipment and integrated solutions. We are dedicated to the design, manufacture, sales and services of solids control systems, following strict quality standards and providing reliable products, professional support and fast response for global customers.
During the past years, together with our experienced engineering team and strong supply chain partners, we have supported drilling contractors, oilfield service companies and industry partners across North America, the Middle East, Africa, Russia, South America, Southeast Asia and other regions, delivering efficient solids control solutions for various drilling operations.
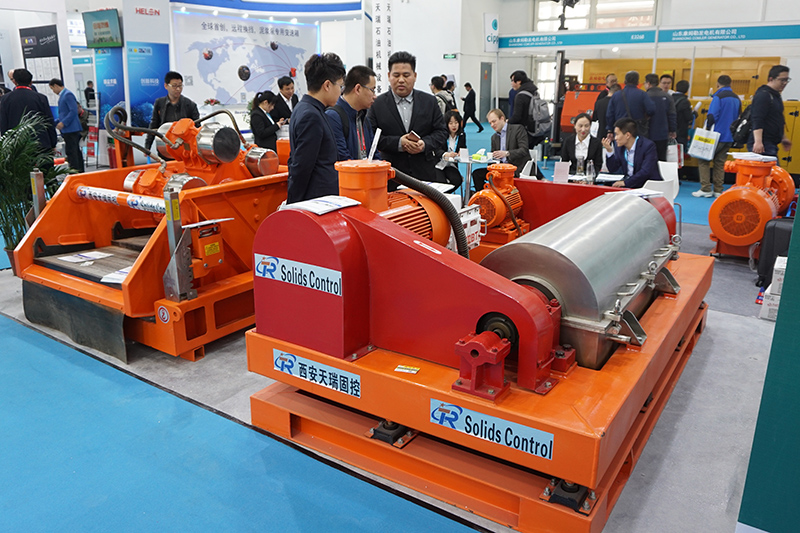
From extreme summer heat in West Texas to sub-zero winter freeze in North Dakota and trenchless urban utility corridors, our systems are built to run 24/7 without unexpected downtime.
High-density multi-well pad drilling requires rapid rig skidding and ultra-high fluid throughput. Our modular mud tank systems feature quick-connect fluid manifolds, explosion-proof centralized electrical panels (UL/NEMA compliant options), and heavy-duty sand traps configured for high ROP (rate of penetration).
Cold climate operations demand integrated steam heating coils, insulated tank walls, freeze-resistant slurry pump seals, and heavy-grade low-temperature structural steels (Q345D/E) that prevent brittle fracturing during harsh North Dakota winter drilling operations.
Large-scale fiber-optic laying, municipal water pipeline boring, and gas pipeline river crossings across the US rely on our compact HDD Mud Recycling units. High portability, rapid site setup, and low acoustic footprints make them ideal for urban job sites.
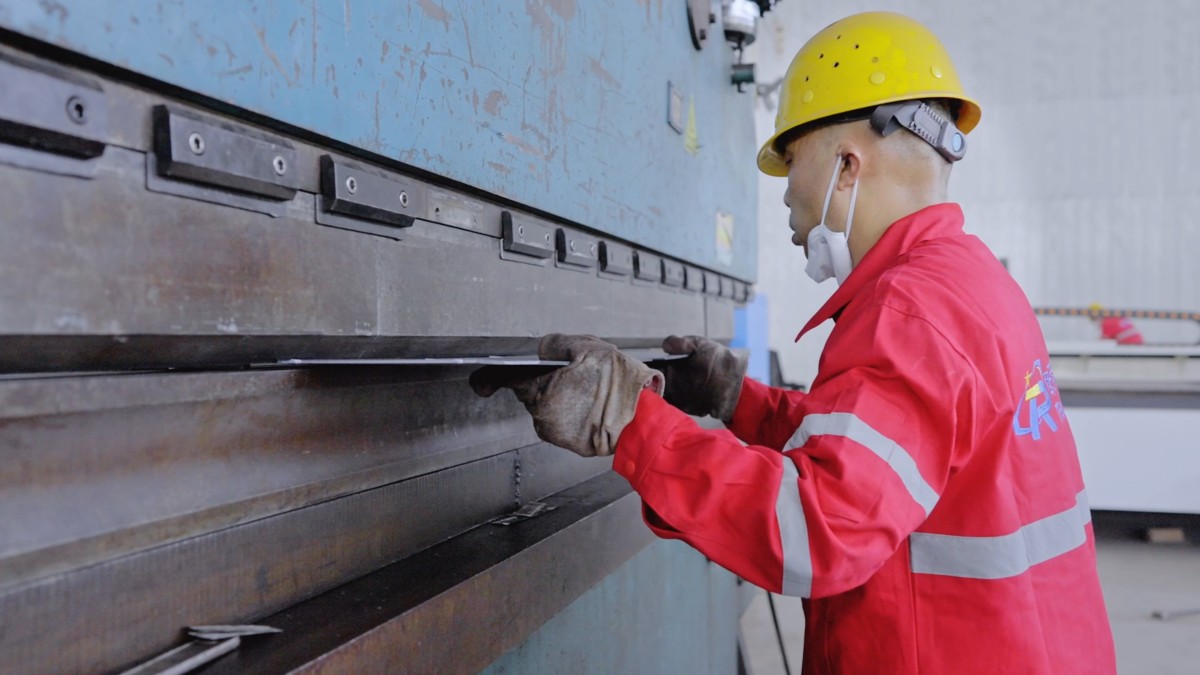
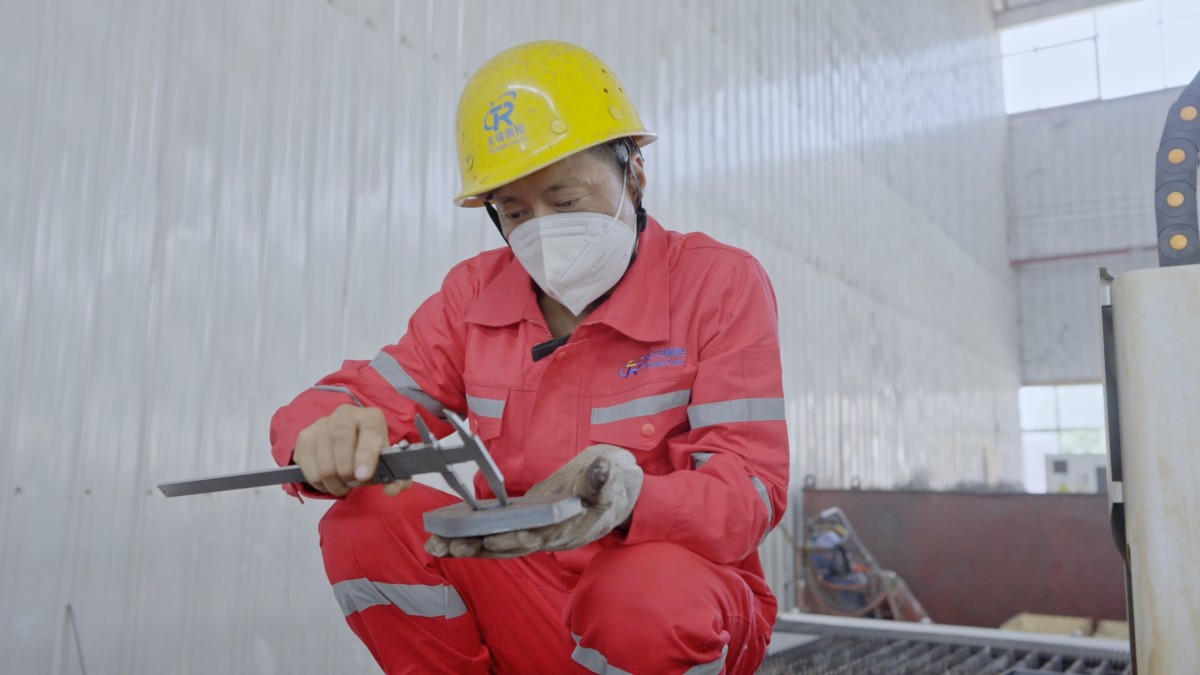
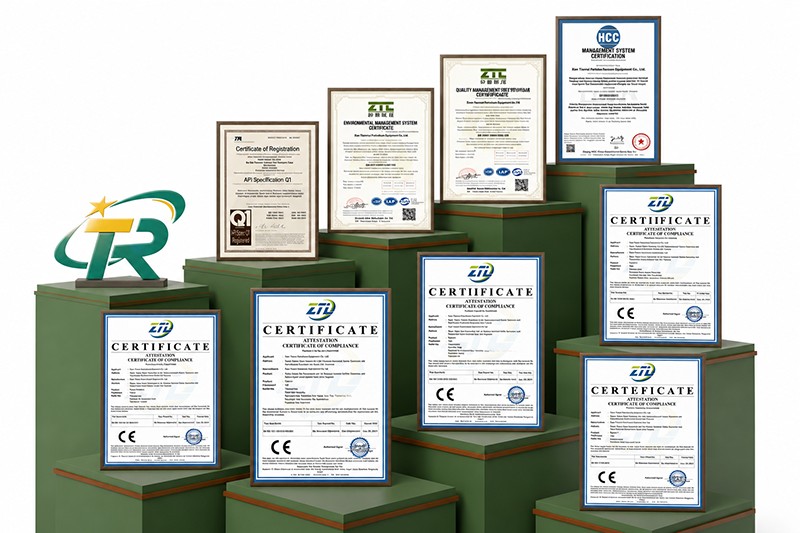
With advanced CNC cutting, automatic submerged arc welding, dynamic balancing, and comprehensive load testing, we guarantee each solids control unit meets the highest international oilfield criteria.
Discover our full line of solids separation, fluid handling, and drilling waste management systems manufactured to exacting standards for US drilling operators, supply houses, and equipment rental fleets.
Integrated compact mud cleaning unit designed for horizontal directional drilling, civil piling, micro-tunneling, and trenchless mud recycling applications.
Continuous screw auger cuttings transfer system fabricated with wear-resistant flighting and high-torque explosion-proof drives for land rigs.
Total closed-loop OBM cuttings treatment system recovering valuable synthetic mud bases and lowering disposal costs below strict regulatory thresholds.
First-stage high-G solids removal shaker engineered for gummy clays and heavy mud volumes, delivering fast fluid conveyance and dry discharge.
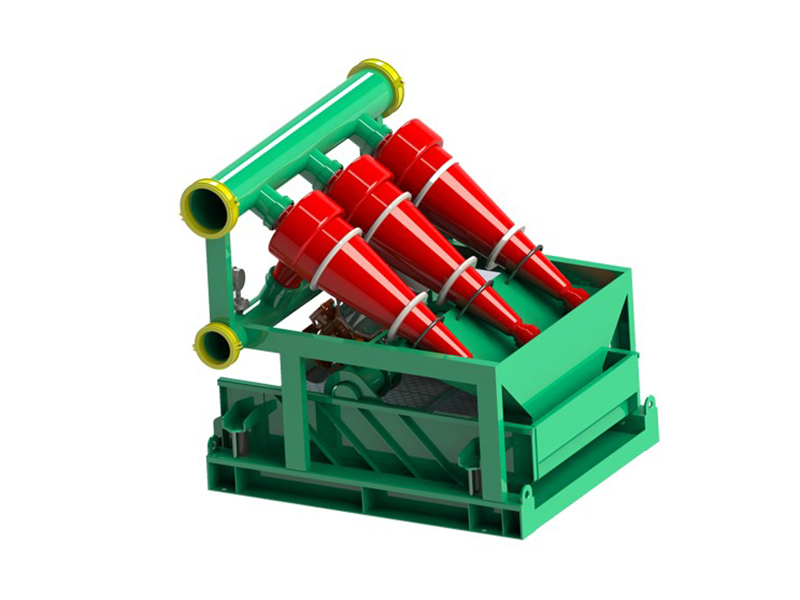
Second-stage hydrocyclone desanding assembly removing sand particulates from 45 to 74 microns, protecting downstream mud pumps and equipment.
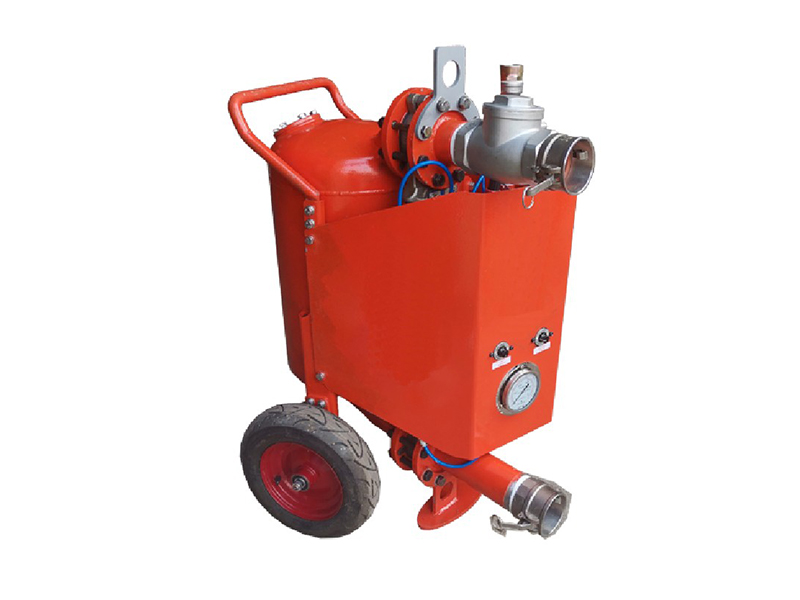
100% pneumatic high-vacuum transfer pump capable of moving heavy sludges, viscous muds, sand slurry, and oilfield waste across long distances.
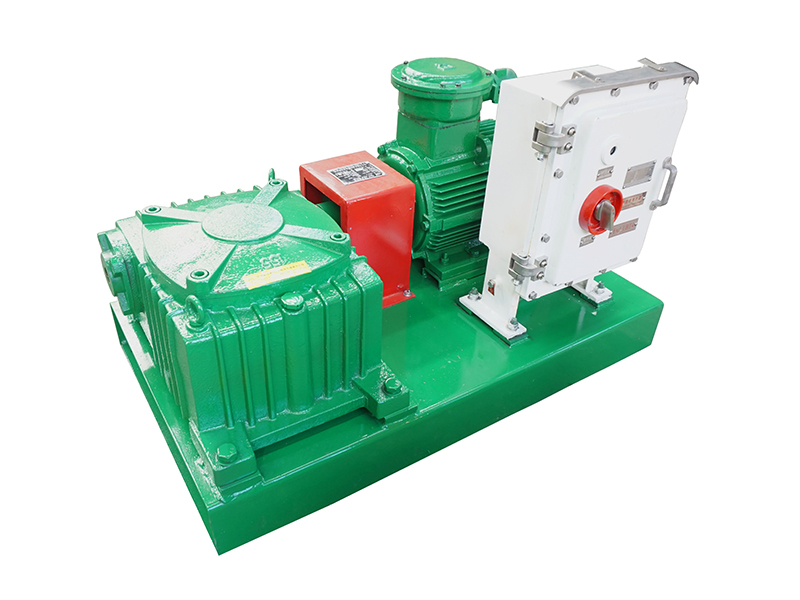
Worm-gear and helical-bevel mud tank agitator preventing weighting solid sedimentation and sustaining homogeneous fluid rheology throughout the system.
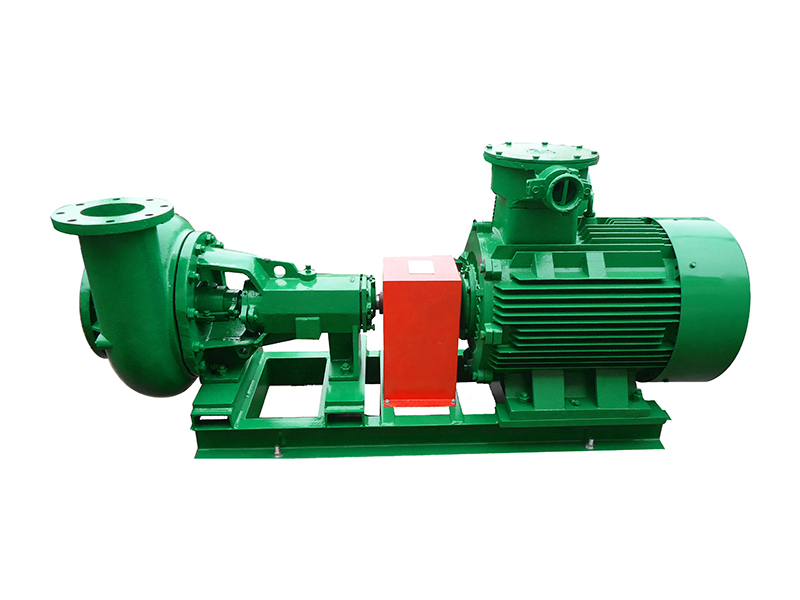
Heavy-duty Mission-style open impeller centrifugal pump supplying uninterrupted feed slurry to desanders, desilters, and mud jet mixing hoppers.
Addressing key questions regarding electrical certifications, logistics shipping cycles to Houston / US Gulf ports, and customized skidding options.
A: Yes. All our electrical motors, vibrators, and control panels can be outfitted with Class I, Div 1 / Class I, Div 2 explosion-proof certifications, UL-listed electrical components, and standard US voltage/frequency configurations (460V/60Hz or 480V/60Hz, 3-Phase).
A: Absolutely. We manufacture API RP 13C compliant composite frame and steel frame replacement screens engineered for seamless fitment on our proprietary shakers as well as standard global OEM shaker models used across North American rigs.
A: Standard standalone components (shakers, pumps, agitators) are generally held in production stock with 15-20 days factory dispatch. Complete turnkey mud tank systems are fabricated within 30-45 days. Direct ocean shipping to Houston, TX or Long Beach, CA typically takes 22-30 days.
A: Yes, our engineering team uses 3D SolidWorks modeling to customize tank dimensions, manifold headers, walkway staircases, and crimped tank wall thicknesses according to your rig sub design and highway transport dimensional limits.