

Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat
Engineered to meet rigorous North American environmental standards (EPA RCRA Subtitle C) and harsh drilling conditions across Texas, New Mexico, North Dakota, and offshore Gulf of Mexico operations.
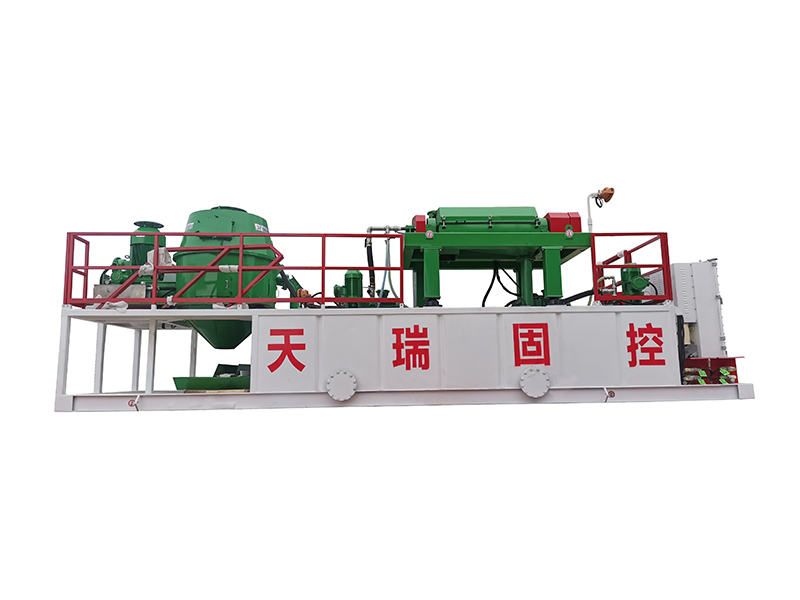
How stringent Environmental Protection Agency (EPA) rules and North American ESG mandates are reshaping oily hazardous waste recovery.
The United States remains one of the largest oil and gas producers in the world, with major unconventional shale plays such as the Permian Basin (Texas/New Mexico), Bakken Formation (North Dakota), Eagle Ford, and Marcellus generating millions of barrels of oily drill cuttings, tank bottom sludge, and production sediment annually. Coupled with extensive downstream petrochemical infrastructure along the US Gulf Coast (Houston, Port Arthur, Corpus Christi, and Louisiana refining corridors), the demand for modular, high-throughput oily waste processing systems has reached unprecedented levels.
Historically, significant portions of oily sludge were managed via landfill disposal, land farming, or deep-well injection. However, escalating disposal fees, tightening environmental liability under the Comprehensive Environmental Response, Compensation, and Liability Act (CERCLA / Superfund), and Resource Conservation and Recovery Act (RCRA) Subtitle C hazardous waste guidelines have made on-site closed-loop waste minimization the imperative standard for US operators.
Modern Chinese oil sludge processing units engineered by TR Solids Control allow American oilfield service companies (OFSCs) and environmental remediators to recover up to 95-98% of clean hydrocarbons from waste sludge. The recovered light and medium crudes are returned directly to the pipeline network or refinery crude distillation units (CDU), creating a profitable secondary revenue stream that rapidly amortizes capital expenditures (CAPEX).
Integrated Allen-Bradley and Siemens PLC architecture enabling real-time torque feedback, differential speed auto-adjustment in decanter centrifuges, and intelligent chemical dosing based on inlet turbidity and solids loading.
All motors, control cabinets, dynamic switches, and junction enclosures comply with UL/CSA standards and ATEX/IECEx certifications, ensuring safe 24/7 continuous operation inside hazardous oilfield and refinery atmospheres.
Containerized, trailer-mounted, and compact modular footprints engineered specifically for standard US Department of Transportation (DOT) flatbed transport between multi-well drilling pads and remote remediation acreage.
Tailored engineering configurations designed for upstream drilling operations, midstream pipeline hubs, downstream refineries, and Superfund environmental restoration.
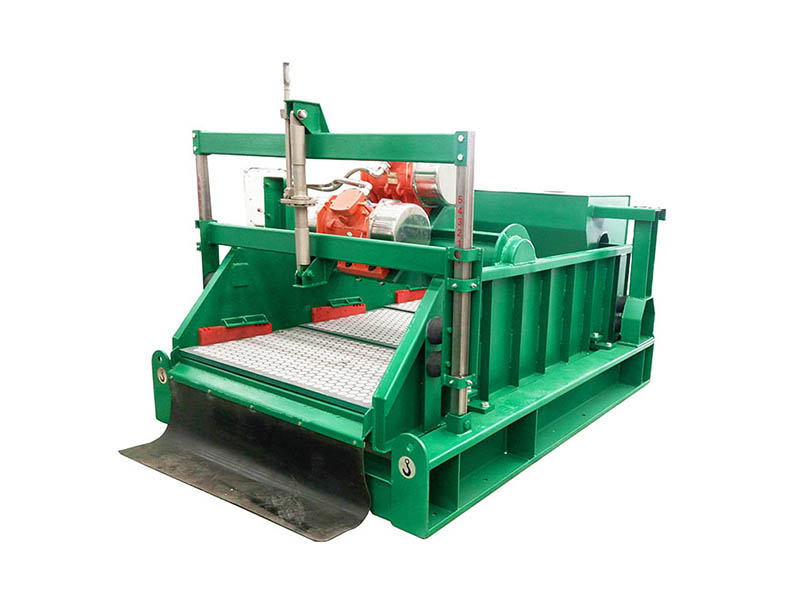
Drilling high-angle lateral wells in West Texas and Southeastern New Mexico produces massive quantities of synthetic and oil-based mud (OBM) cuttings. Our specialized high G-force drying shakers and decanter centrifuges strip synthetic base oils down to less than 1% retained fluid, returning expensive diesel/mineral oils back to the mud system while rendering dried rock cuttings harmless for roadbed stabilization or pitless disposal.
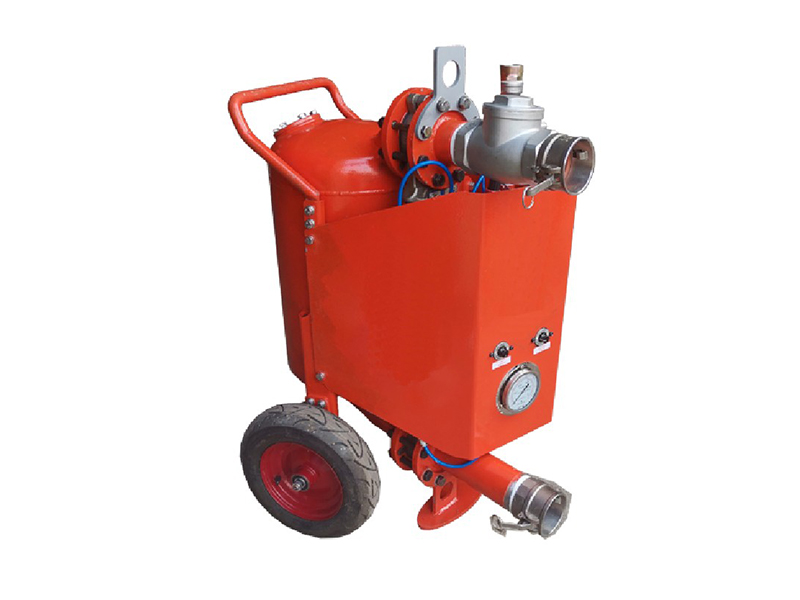
Crude oil storage tanks along the Texas and Louisiana coasts accumulate stubborn asphaltic, paraffinic, and sand-heavy sludge over years of operation. Utilizing our high-vacuum sludge transfer pumps, chemical demulsification skid, hot water wash tanks, and three-phase disc/tricanter centrifuges, operators achieve clean 3-phase separation: saleable crude oil (<0.5% BS&W), clean effluent water, and stackable inert solid cakes.
For historical unlined earthen pits and aged hydrocarbon lagoons across Oklahoma, Ohio, and Pennsylvania, TR Solids Control units provide rugged, self-contained separation trailers with built-in polymer hydration units, macerators, and heavy-duty solids decanters capable of handling abrasive sand, rocks, weathered heavy oils, and biological slimes.
Petrochemical cracking facilities, lubricant blenders, and marine barge cleaning facilities utilize our continuous high-speed decanting systems to dewater dissolved air flotation (DAF) oily scum, minimizing hauling weight and slashing third-party hazardous incineration or treatment costs by up to 70%.
A global leader in drilling fluid solids control equipment and integrated oil sludge treatment solutions.
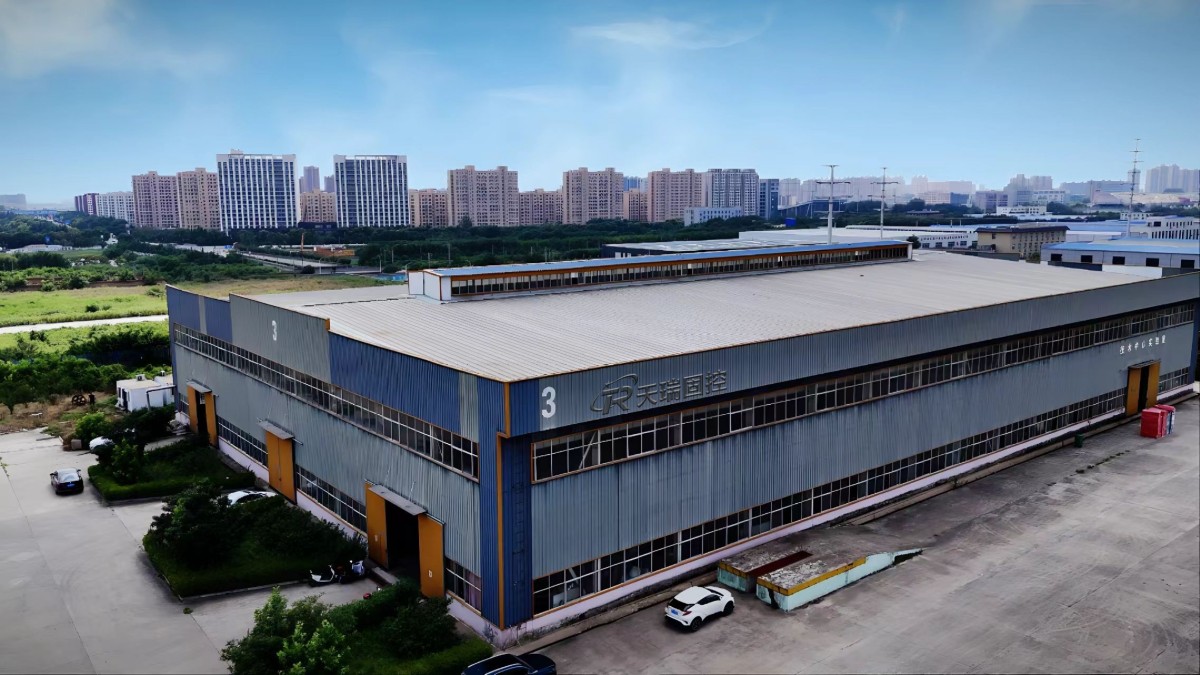
Established in 2010, TR Solids Control is a professional manufacturer specializing in drilling fluid solids control equipment and integrated solutions. We are dedicated to the design, manufacture, sales and services of solids control systems, following strict quality standards and providing reliable products, professional support and fast response for global customers.
During the past years, together with our experienced engineering team and strong supply chain partners, we have supported drilling contractors, oilfield service companies and industry partners across Middle East, Africa, Russia, South America, Southeast Asia and other regions, delivering efficient solids control solutions for various drilling operations.
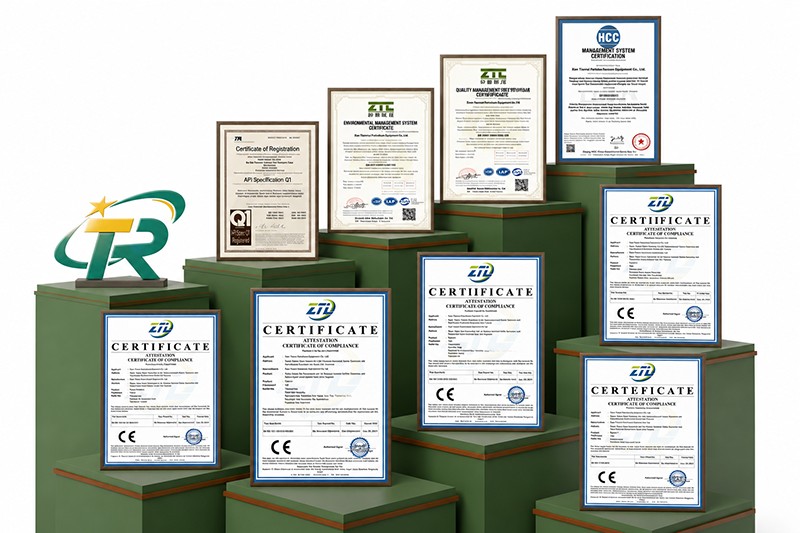
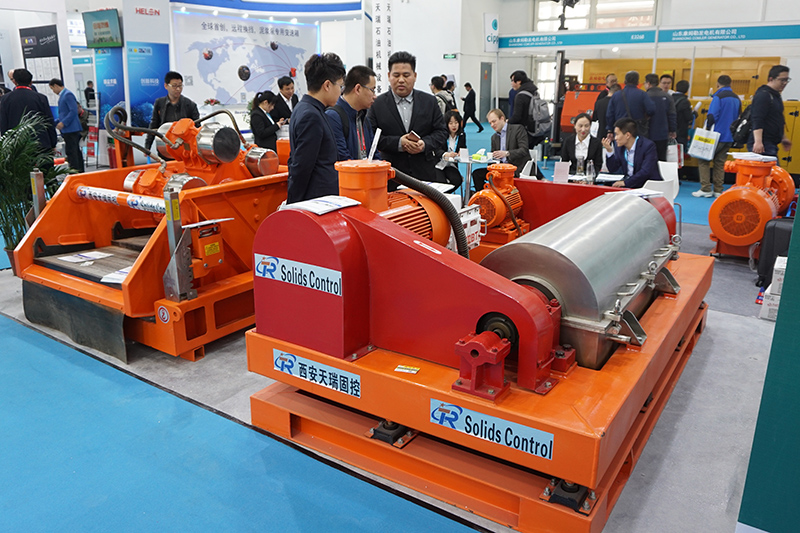
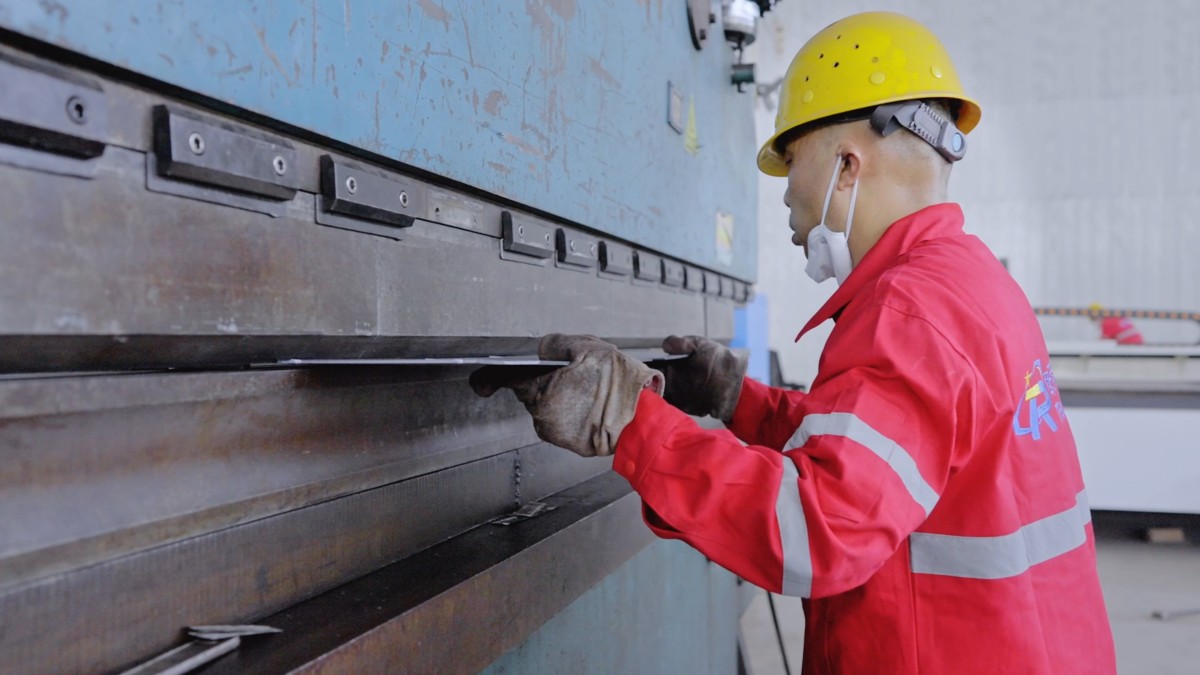
Manufacturing • Engineering • Global Service
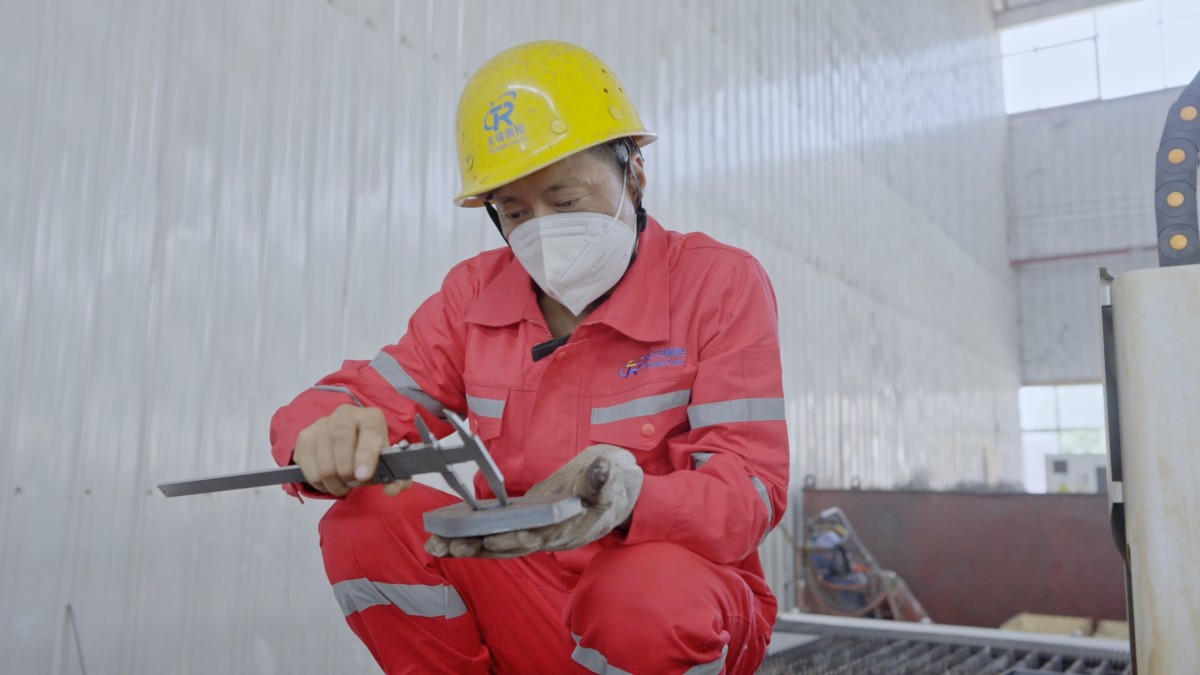
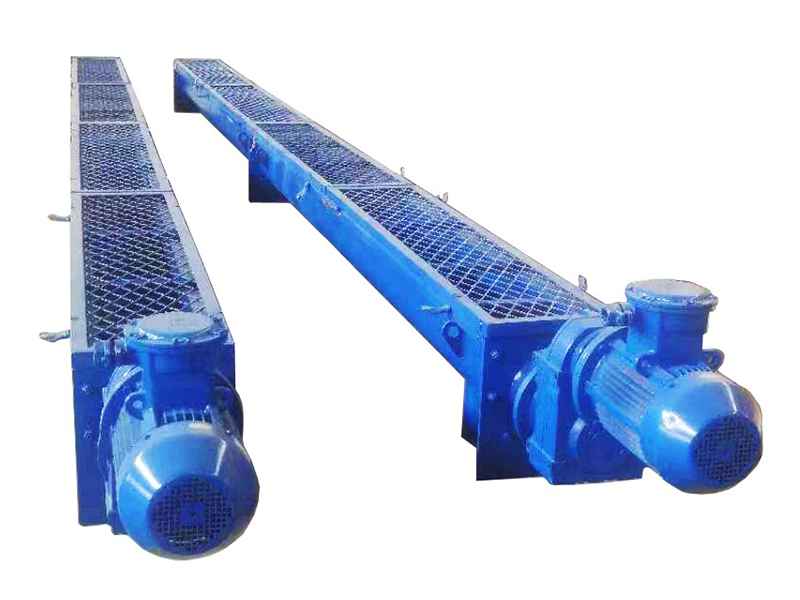
Explore our complete catalog of high-performance mud recovery, sludge transfer, mechanical separation, and drilling fluid processing modules customized for US energy contractors.
Combining heavy engineering craftsmanship, certified API standards, and unmatched cost-efficiency for turnkey oily waste projects.
Navigating the North American competitive energy sector requires suppliers who offer both cutting-edge separation metallurgy and agile manufacturing economics. TR Solids Control provides comprehensive OEM and ODM support for American engineering contractors, drilling firms, and environmental service providers.
Key strategic advantages for US buyers include:
Whether you are treating OBM cuttings in Midland, Texas, remediating storage tank bottoms in Louisiana, or managing DAF oily sludge in the Midwest, our engineering team can custom-configure a 5 m³/h to 50 m³/h modular treatment package.